If you’ve ever waited for a custom-made metal part for a medical device, aerospace component, or a high-performance automotive brake, you know how devastating even a tiny concentricity error can be. Last month, I had a call from a medical equipment engineer who’d spent three months debugging a faulty surgical robot arm—turns out a precision bushing from a cheap overseas supplier was 0.018mm off its target concentricity. That’s less than the width of a human red blood cell, and it was enough to make the robot’s end effector drift during minimally invasive procedures. As a precision metal parts supplier with 18 years working with clients in aerospace, medical, and defense, concentricity isn’t just a spec on a drawing to me—it’s the difference between a product that works as designed and one that causes delays, recalls, or worse. Precision Metal Parts
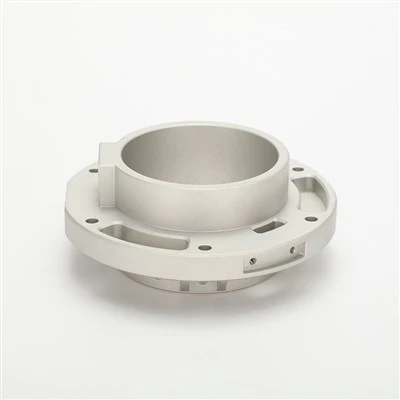
Concentricity, for anyone new to the term, is the measure of how well two or more cylindrical features (like a shaft and its mating bore, or a series of gear teeth around a central axis) share a common central axis. The tolerance is almost always tight for precision parts: most of our clients require concentricity within 0.005mm to 0.02mm, and some military-grade components need it down to 0.002mm. Hit that mark, and parts fit seamlessly, run smoothly, and maintain alignment under load. Miss it, and you get premature wear, vibration, misfits, and catastrophic failure in high-stakes applications.
Over the years, I’ve learned that concentricity errors almost never happen by accident. They’re the result of small, avoidable choices made across the entire production cycle, from part design to final inspection. Let’s break down what actually works to lock in concentricity, with the lessons we’ve tested in our shop floor and the mistakes we’ve fixed for clients.
First, it starts with part design—no amount of good machining will fix a design that sets you up for concentivity drift before you even cut metal. I see this all the time: engineers design a part with a primary feature (say, a central bore) and a secondary feature (like a flange or a mating shaft) that’s supposed to share that axis, but they don’t account for manufacturing constraints. For example, if you’re designing a part with a long internal bore, making it from a single piece of solid bar stock means you’re asking a cutting tool to reach deep into a hole to machine the walls. The longer the tool, the more it bends under pressure, and that deflection will throw off concentricity.
Our go-to fix here when working with clients is design for manufacturability (DFM) reviews, and we never skip them. Last year, a defense client came to us with a rocket actuator pin design that required a 12mm long bore inside a 25mm diameter bar. The original design called for a single boring operation, but our DFM team pointed out that a long, thin boring bar would deflect 0.012mm mid-cut—enough to fail their 0.008mm concentricity spec. Instead, we suggested splitting the part into two smaller pre-machined components that are press-fit and synchronized during final machining, cutting that deflection to less than 0.002mm. The client didn’t have to redesign their whole system, just adjust how the part was built, and they stayed on schedule. Another common design mistake? Not setting a primary datum feature right at the start. The ISO GPS standard says concentricity is measured relative to a datum, so if you pick a datum that’s not a stable, machined feature (like a rough cast edge), you’ll never get consistent measurements. We always push clients to define datums as finished, precision-machined surfaces early in the design stage.
Next, and this is the most overlooked step in our industry: workholding setup that doesn’t introduce concentricity errors. A lot of shops just clamp a part in a vise or a three-jaw chuck, fire up the machine, and assume it’s aligned. That works for parts with loose tolerances, not for precision metal. Let’s talk about what we do differently. For turning operations (where we machine round parts on a lathe), a three-jaw chuck is fine only if it’s true within 0.003mm—and we check that with a dial indicator before every run, even if it’s a new chuck. But for parts with super tight concentricity, we use a collet chuck instead. Collets grip the entire circumference of the part, not just three points, eliminating the “jaw deflection” that throws off roundness and concentricity. We also never use soft jaws for high-precision work without grinding them to match the part’s outer diameter. If your soft jaws are made generic, they’ll have tiny deviations in their grip that translate directly to concentricity error. Every time we change a part lot or a batch size, we re-grind soft jaws to within 0.002mm of the part’s OD.
For milling operations, where we machine non-round or multi-feature parts, we use vacuum chucks and customized fixture plates that are machined right at our shop. Last quarter, we had a client that made valve bodies for medical inhalers—each part had three radial bores that needed to be concentric to within 0.005mm. The original fixture they were using was a generic off-the-shelf plate that shifted 0.007mm when the milling tool plunged into the part. We custom-machined a fixture that had precision locating pins that mated to the part’s pre-machined datum feature, and bolted the part down so there was zero movement during cutting. The result? We hit their spec on every first-run part, no rework needed. Another workholding tip: we never hold a part by its finished, precision-machined surface. We use soft jaws, custom locators, or sacrificial stock features (called “ears” or “tangs”) that we machine off after production. If you clamp a finished bore that’s already within spec, you’ll deform it just enough to push concentricity out of tolerance by the time you’re done machining the mating feature.
Then there’s machining process control—and this is where a lot of shops cut corners, and it’s how we stay consistent. Let’s start with tooling. A dull cutting tool doesn’t just leave a bad surface finish—it generates extra vibration and cutting pressure that deflects the tool or the part, throwing off concentricity. We change all tools according to a rigorous schedule, not just when they look dull. For high-precision boring operations, we use solid carbide boring bars with coolant-through holes, not HSS (high-speed steel) bars. The coolant flows directly to the cutting edge, keeps the tool at a consistent temperature, and reduces deflection. We also machine parts in stages: first rough cut, then semi-finish, then finish. Rough cutting removes most of the material, but it also puts a lot of stress on the part, making it distort slightly. If you finish a part right after roughing, that residual distortion will show up as concentricity error. We let parts “soak” after roughing and semi-finishing—leave them on the shop floor for at least 4 hours to release internal stress—before doing the final finish pass. That simple step alone cut our concentricity rework rate by 12% last year.
Temperature control is another big one I don’t hear enough about. Machine shops get hot—lighting, cutting tools, and the machine itself can raise the ambient temperature by 10 degrees or more during a shift. Metal expands when it’s hot, contracts when it’s cold. If you machine a part when the machine spindle is warm, then inspect it later when it’s cooled down, you’ll get a concentricity error that’s not from bad machining at all—it’s from thermal expansion. We’ve invested in climate control for our precision machining bays, keeping the temperature within ±1 degree Celsius 24/7. For parts that need the absolute tightest tolerances, we even machine and inspect them at the same stable temperature, using granite surface plates that also match the shop’s ambient temperature. I once had a client who machined a small gear for a satellite and got a 0.010mm concentricity error that they couldn’t explain until we checked: their shop temperature fluctuated 8 degrees between day and night, and the thermal shift of the machine tool was enough to throw their measurements off. Fixing the shop’s climate control solved their problem.
Then there’s inspection—you can’t control what you don’t measure, and for concentricity, generic calipers won’t cut it. We use coordinate measuring machines (CMMs) with contact probes that have a resolution of 0.0001mm, plus specialized concentricity gages for high-volume or rapid checks. But here’s the thing about inspection: you have to measure the same datum you defined in your drawing, and you have to measure multiple points around the circumference, not just two. A lot of shops only measure two points on a bore to check concentricity, but if those points are on opposite sides, you’ll miss a tiny off-center deviation that’s only present at a specific angle. We measure at least 8 equidistant points around each feature, and we run a full CMM report for every part batch that goes to aerospace or medical clients. We also do in-process checks, not just at the end. Every 10 parts, we pull one off the machine mid-production to check concentricity, so if a tool starts to wear or a fixture shifts, we catch it before we make a whole batch of bad parts. Last month, we caught a worn collet in the middle of a run, and the in-process check showed a 0.006mm concentricity drift—if we’d waited to the end, we would’ve had 20 bad parts to scrap, instead of just one.
Wait, I should also mention the human factor. This isn’t just a list of machines and processes—it’s about the people running them. Our machinists aren’t just operators; they’re trained to spot small changes that lead to concentricity errors. We do weekly training sessions where we review parts that passed or failed, talk about why a concentricity spec mattered for the client’s application, and practice adjusting setups. Early in my career, I worked with a machinist named Carlos who taught me that the best part of a run isn’t the first part—it’s the 10th. The first part might feel aligned, but after a few cuts, the tool settles, the chuck grips tighter, and the concentricity hits its mark. That lesson stuck with me: we never ship a first-run part, we always run at least 10 pieces and inspect the middle or end of the batch to ensure consistency.
Let’s be real—no process is perfect, even for the best suppliers. But what separates precision metal parts suppliers is how they mitigate those small risks. I’ve seen shops cut corners on DFM, use old chucks, skip in-process checks, and still get lucky with simple parts. But when you’re making parts that go into a pacemaker, a jet engine, or a satellite, luck isn’t a strategy. It’s why we don’t chase low-cost orders; we specialize in the parts where concentricity isn’t just a spec, it’s a safety requirement.
If you’re an engineer or a procurement manager dealing with precision metal parts, don’t wait for a failed prototype or a production delay to think about concentricity. Ask your supplier: what’s their process for workholding setup? Do they do DFM reviews before quoting? What’s their inspection method, and do they have in-process checks? For us, these aren’t trick questions—they’re the foundation of how we do business. We’ve had clients come to us after bad experiences with other suppliers, and 9 times out of 10, the problem wasn’t that the supplier couldn’t machine to the spec, it was that they cut corners on the steps that actually prevent concentricity error.
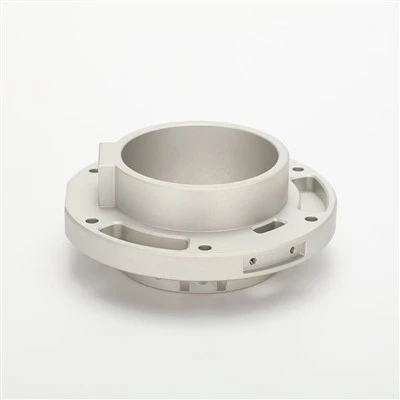
At the end of the day, concentricity is about consistency. It’s about every single part from a batch meeting the same tight tolerance, every time. That’s what our team has built our business on over the last 18 years. If you’re working on a project that needs precision metal parts with tight concentricity, let’s connect to talk through your requirements, troubleshoot design challenges, and make sure your parts meet your specs on time.
Plastic Injection Molding for Electronics References
- ASME Y14.5-2018, Dimensioning and Tolerancing, American Society of Mechanical Engineers
- ISO 12180-2:2011, Geometrical Product Specifications (GPS) – Cylindricity – Part 2: Specification operators, International Organization for Standardization
- Smith, G. T. (2020). Fundamentals of Modern Manufacturing: Materials, Processes, and Systems (7th ed.). Wiley
- DeGarmo, E. P., Black, J. T., & Kohser, R. A. (2022). DeGarmo’s Materials and Processes in Manufacturing (14th ed.). Pearson
Zhejiang Hayi Technology Co., Ltd.
With abundant experience, we are one of the most professional precision metal parts manufacturers in China. We warmly welcome you to wholesale bulk precision metal parts in stock here and get quotation from our factory. All customized products are with high quality and competitive price.
Address: Room 112, 1st Floor, No. 103, Siwangdai, Pingzhai Village, Renhe Subdistrict, Yuhang District, Hangzhou City, Zhejiang Province
E-mail: 18368133797@163.com
WebSite: https://www.zhejianghayi.com/
