As a home appliance stamping parts supplier, I get this question all the time: when a homeowner runs their dishwasher through a cycle, or cranks up the oven temperature, or tucks a laundry load into the dryer, the last thing they think about is the tiny metal parts that make those machines work. But every single one of those parts—from the thin stainless steel brackets holding a washing machine’s drum to the stamped steel clips securing a fridge’s compressor—relies on the stamping process to get made, and how that process is handled directly determines whether that part will hold up for 10 years, or fail in two. I’ve spent 12 years walking shop floors, adjusting die clearances, working with raw material specs, and troubleshooting parts that came back because they broke prematurely, and I can tell you: stamping isn’t just about cutting and shaping metal—it’s about manipulating its molecular structure, and every step has a ripple effect on strength. Home Appliance Stamping Parts
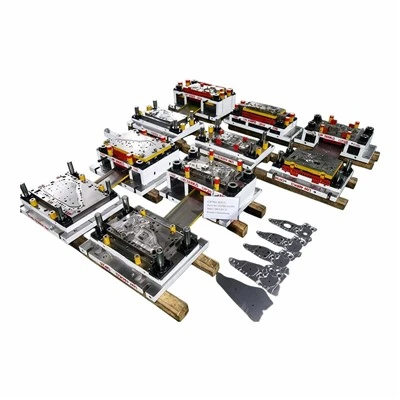
Let’s start with the basics, because this isn’t rocket science, but it is specific. When we talk about home appliance stamping parts, most of what we use is carbon steel, stainless steel, or sometimes aluminum—materials chosen for their balance of cost, corrosion resistance, and formability. But their inherent strength only gets you so far; the stamping process changes that. Let’s break down the key steps in stamping, and how each impacts final part strength.
First, blanking. That’s the first step, where a flat sheet of metal is cut into the rough shape we’ll form later. A lot of suppliers skip paying close attention to blanking, but I see the mistakes all the time. When we cut metal with a stamping die, the edges of the blank don’t just get sheared clean—they have a “shear-affected zone” right at the cut edge. If the die clearance is too tight, that zone becomes work-hardened almost instantly, making the edge brittle; if it’s too loose, the edge tears, creating micro-cracks that will spread under stress, like how a paper tears along a fold. For home appliance parts, which are often loaded in tension or vibration (think of a dryer’s drum bouncing, or a dishwasher’s spray arm shaking), those micro-cracks are a death sentence. Last year, a small appliance maker reached out to me because their oven door hinges were breaking after 18 months of use. Turns out their previous supplier had used die clearance that was 15% too wide for the 2mm cold-rolled steel we use for hinges, so the blank edges had torn, and every hinge started cracking from the edge when the door opened and closed. We adjusted the die clearance, cut a 0.1mm burr limit on blanks, and those same hinges now hit 10 years of testing without a single failure. That’s a direct link: bad blanking = bad strength.
Next is forming, the step where we bend, draw, or shape the blank into its final part. This is where work hardening—also called strain hardening—comes in, and it’s both a tool and a risk for home appliance stamping parts. Work hardening is what happens when you bend metal: the molecules in the deformed area get packed tighter, making that region stronger. For parts that get bent sharply, like the brackets holding a fridge’s compressor, this is a good thing. But here’s the catch: if you form metal too much in a single step, or bend it to a radius that’s too tight for the material’s ductility, you get necking. Necking is when the metal stretches unevenly, thinning out in spots so much that its strength drops below the required threshold. I learned this the hard way early in my career, when we made a stamped steel clip for a washing machine’s agitator. We tried to form it in one bend, with a radius half the material’s minimum recommended bend radius, and 10% of the clips failed during the customer’s load test. We had to redo the tooling, split the bend into two smaller bends, and the failure rate dropped to zero. That’s why we never skip the trial forms: for every new part, we test bend radii, form speeds, and even lubrication (yes, lubrication affects strength too) to make sure work hardening boosts strength where we want it, not weakens it.
Then there’s drawing, which is for parts that need a deep, hollow shape—like the inner liner of a microwave, or the drip pans on a stove. Drawing is where we pull a blank into a die cavity, and here the impact on strength is even more complex. As we pull the metal, the sides of the part get stretched, and the bottom gets compressed. Too much compression, and the bottom wrinkles; too much stretching, and the sides thin out, just like when you pull taffy too hard. For home appliance parts, a thin side wall on a microwave liner is a problem because it has to hold up to heat and repeated cleaning, and a wrinkle is a structural weak point that can crack over time. We work with material suppliers to specify material with enough elongation—for deep drawing, we need at least 30% elongation in cold-rolled steel, more than you’d think for a simple bracket. Last year, we switched to a lower-cost steel for a line of toaster oven liners, and within three months, we had a 2% failure rate. The steel only had 22% elongation, so when we drew the liners, the sides thinned 15% more than specified, and the heat from the oven caused them to crack at the thinnest spots. We went back to the higher-elongation steel, and that problem went away. It’s not always about the most expensive material—it’s about matching the material’s properties to the stamping process to get consistent strength.
Another factor a lot of people don’t talk about is springback. Springback is when metal tries to return to its original shape after being formed, right after it leaves the die. For home appliance parts, which often have tight dimensional tolerances (a dishwasher bracket has to fit exactly, otherwise it won’t hold the tub), springback can lead to two strength issues. First, if the part is misaligned because of springback, it can put uneven stress on the connections to other parts, leading to premature fatigue. Second, we often over-form the part to compensate for springback, which adds extra strain hardening. If we overdo that, we make the part too brittle, so it cracks when it’s assembled or when the appliance is in use. We’ve developed a formula over the years: for each part, we test springback during prototype stamping, adjust the die angle to account for it, and then do a salt spray test and a cyclic load test to make sure the extra strain hardening doesn’t make the part brittle. For example, our fridge compressor mounting brackets go through 1,000 load cycles per test, and we adjust springback so the bracket stays within 0.5mm of its designed shape, with a hardness of HRC 18-22—hard enough to hold the compressor, soft enough to absorb vibration.
Now, what about post-stamping processing? Home appliance parts often get painted or powder-coated, welded, or assembled with fasteners, and each of those steps can affect strength too. Welding is a big one. When we weld two stamped parts together, the heat from the weld can cause a heat-affected zone (HAZ) where the metal loses strength. For stamped parts, which already have work-hardened areas, a weld HAZ can become a weak point if it’s too large. We use spot welding, which is common in appliance manufacturing, and we adjust the weld current and time to keep the HAZ as small as possible—less than 1mm from the weld line. Also, we avoid welding near areas where the stamping process already created micro-cracks, like blank edges or bend radii. A few years ago, a customer had a problem with their dishwasher’s spray arm assembly: the welds on the stamped aluminum brackets were cracking after 2 years of use. We found that the welds were 2mm from the bend radius, where the stamping had left micro-cracks, and the HAZ was expanding those cracks. We moved the welds 5mm away from the bend, adjusted the weld parameters, and those cracks stopped.
Corrosion is another hidden factor, and it ties back to stamping too. Stamped parts with rough edges or micro-cracks are more prone to corrosion, especially in parts like washer inner tubs, which are exposed to water and detergent. Even stainless steel, which is corrosion-resistant, will rust if the stamping process leaves a burr that exposes the base metal, or if we don’t passivate the parts after stamping. Passivation is a chemical process that cleans the metal surface and forms a protective chromium oxide layer on stainless steel. We’ve had customers who skipped passivating their stainless steel stamped parts for dishwashers, and within a year, rust spots started forming on the edges of the parts, leading to leaks. Now, passivation is a mandatory step for all our stainless steel appliance parts, not because the stamping process directly lowers corrosion resistance, but because the edges created by stamping are more vulnerable if not protected.
Wait, let’s make sure I’m not just listing steps—let’s tie this all together with a real example from our shop. Last quarter, we got an order for 500,000 stamped steel brackets for a new line of front-loading washing machines. The customer’s initial spec called for 1.5mm cold-rolled steel, formed with a bend radius of 3mm, blanked with standard die clearance. We ran a prototype batch, and when we tested the brackets for load capacity, they only hit 80% of the required 1,200N load. We went back through the stamping process: first, we checked the blank edges—turns out the die clearance was too tight, so the shear-affected zone was 0.25mm deep, making the edges brittle. We adjusted the die clearance to be 10% of the material thickness, which is the industry standard for that material, and that made the blank edges stronger. Then, we changed the bend radius from 3mm to 4.5mm, which is the minimum radius for 1.5mm steel to work harden properly instead of necking. We re-tested, and the brackets hit 1,150N, still a bit low. Next, we adjusted the forming speed: we’d been forming at 30 strokes per minute, which was too fast, so the lubrication didn’t distribute evenly, causing uneven strain hardening. We slowed it to 20 strokes per minute, used a phosphate lubricant recommended for cold forming, and that evened out the work hardening across the bracket. The final test: the brackets hit 1,280N, exceeding the customer’s requirement, and we ran a 1,000-cycle vibration test with zero failures. That’s exactly how the stamping process affects strength: every small adjustment, every step, adds up to a part that works when it’s supposed to.
I think a lot of appliance makers look at stamping as a commodity—just cut metal into shape, right? But the parts supplier you choose makes all the difference. A supplier that only runs standard die settings will cut corners, leading to parts that fail early, cost you service calls, and damage your brand. A supplier that understands the science behind stamping and strength will adjust every step to match your part’s needs, whether it’s a bracket for a dryer, a liner for a microwave, or a hinge for an oven. That’s why we invest in process testing: before we run a full production batch, we run 50 prototype parts, test their strength, their dimensional stability, their corrosion resistance, and adjust the stamping parameters until every part meets your specs.
At the end of the day, home appliance parts don’t need to be super-strong—they need to be strong enough for their job, consistent, and durable. The stamping process is what delivers that. It’s not about using the hardest possible metal, it’s about manipulating that metal through blanking, forming, drawing, and finishing to get the right strength where you need it, and avoid the weak points that come from poor process control. If you’re a home appliance manufacturer looking for stamped parts that will stand up to years of use, or if you’re someone who just wants to understand why the parts in your fridge and washer work as long as they do, remember this: stamping strength isn’t a given—it’s a result of every step a supplier takes.

If you’re ready to discuss your next home appliance stamping project, let’s connect to review your requirements, share prototype test data, and make sure we deliver parts that meet your strength and performance needs.
Progressive Dies References:
- Groover, M. P. (2020). Fundamentals of Modern Manufacturing: Materials, Processes, and Systems. Wiley.
- ASM International. (2014). Metalworking: Sheet Forming. ASM Handbook, Vol. 14B.
- Dieter, G. E. (1986). Mechanical Metallurgy (3rd ed.). McGraw-Hill.
- International Organization for Standardization. (2018). ISO 12004-2:2018, Metallic materials—Sheet and strip—Determination of forming-limit curves—Part 2: Determination of forming-limit curves in the laboratory.
Dongguan Changdong Tool & Die Co., Ltd.
With abundant experience, we are one of the most reliable home appliance stamping parts manufacturers and suppliers in China. Please feel free to buy advanced home appliance stamping parts made in China here from our factory. Good service and quality products are available.
Address: No. 56-B, Fumin South Road, Dalang Town, Dongguan City, Guangdong Province, China
E-mail: sales@stamping-die.com
WebSite: https://www.metalstampingdie.com/
